Market Applications
Refrigeration Pumps
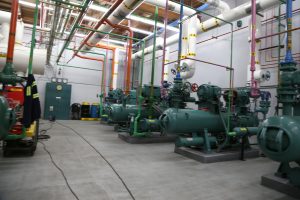
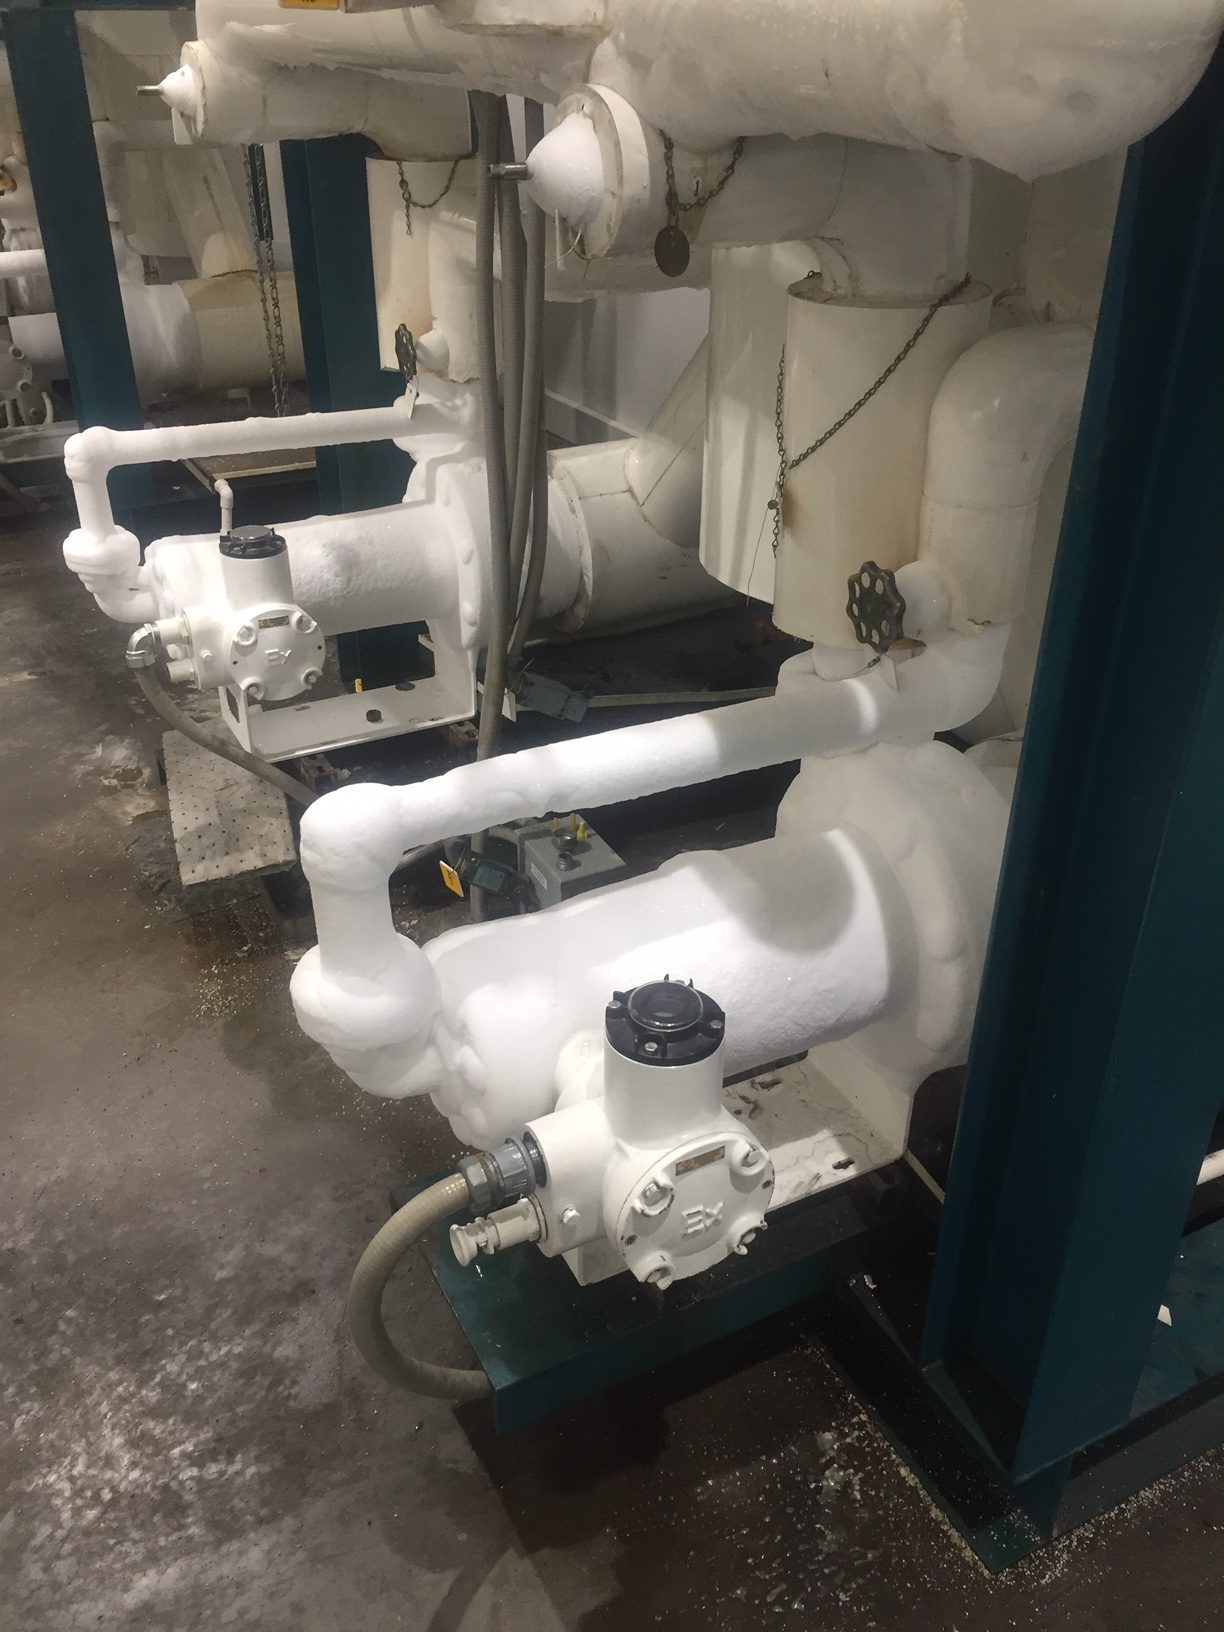
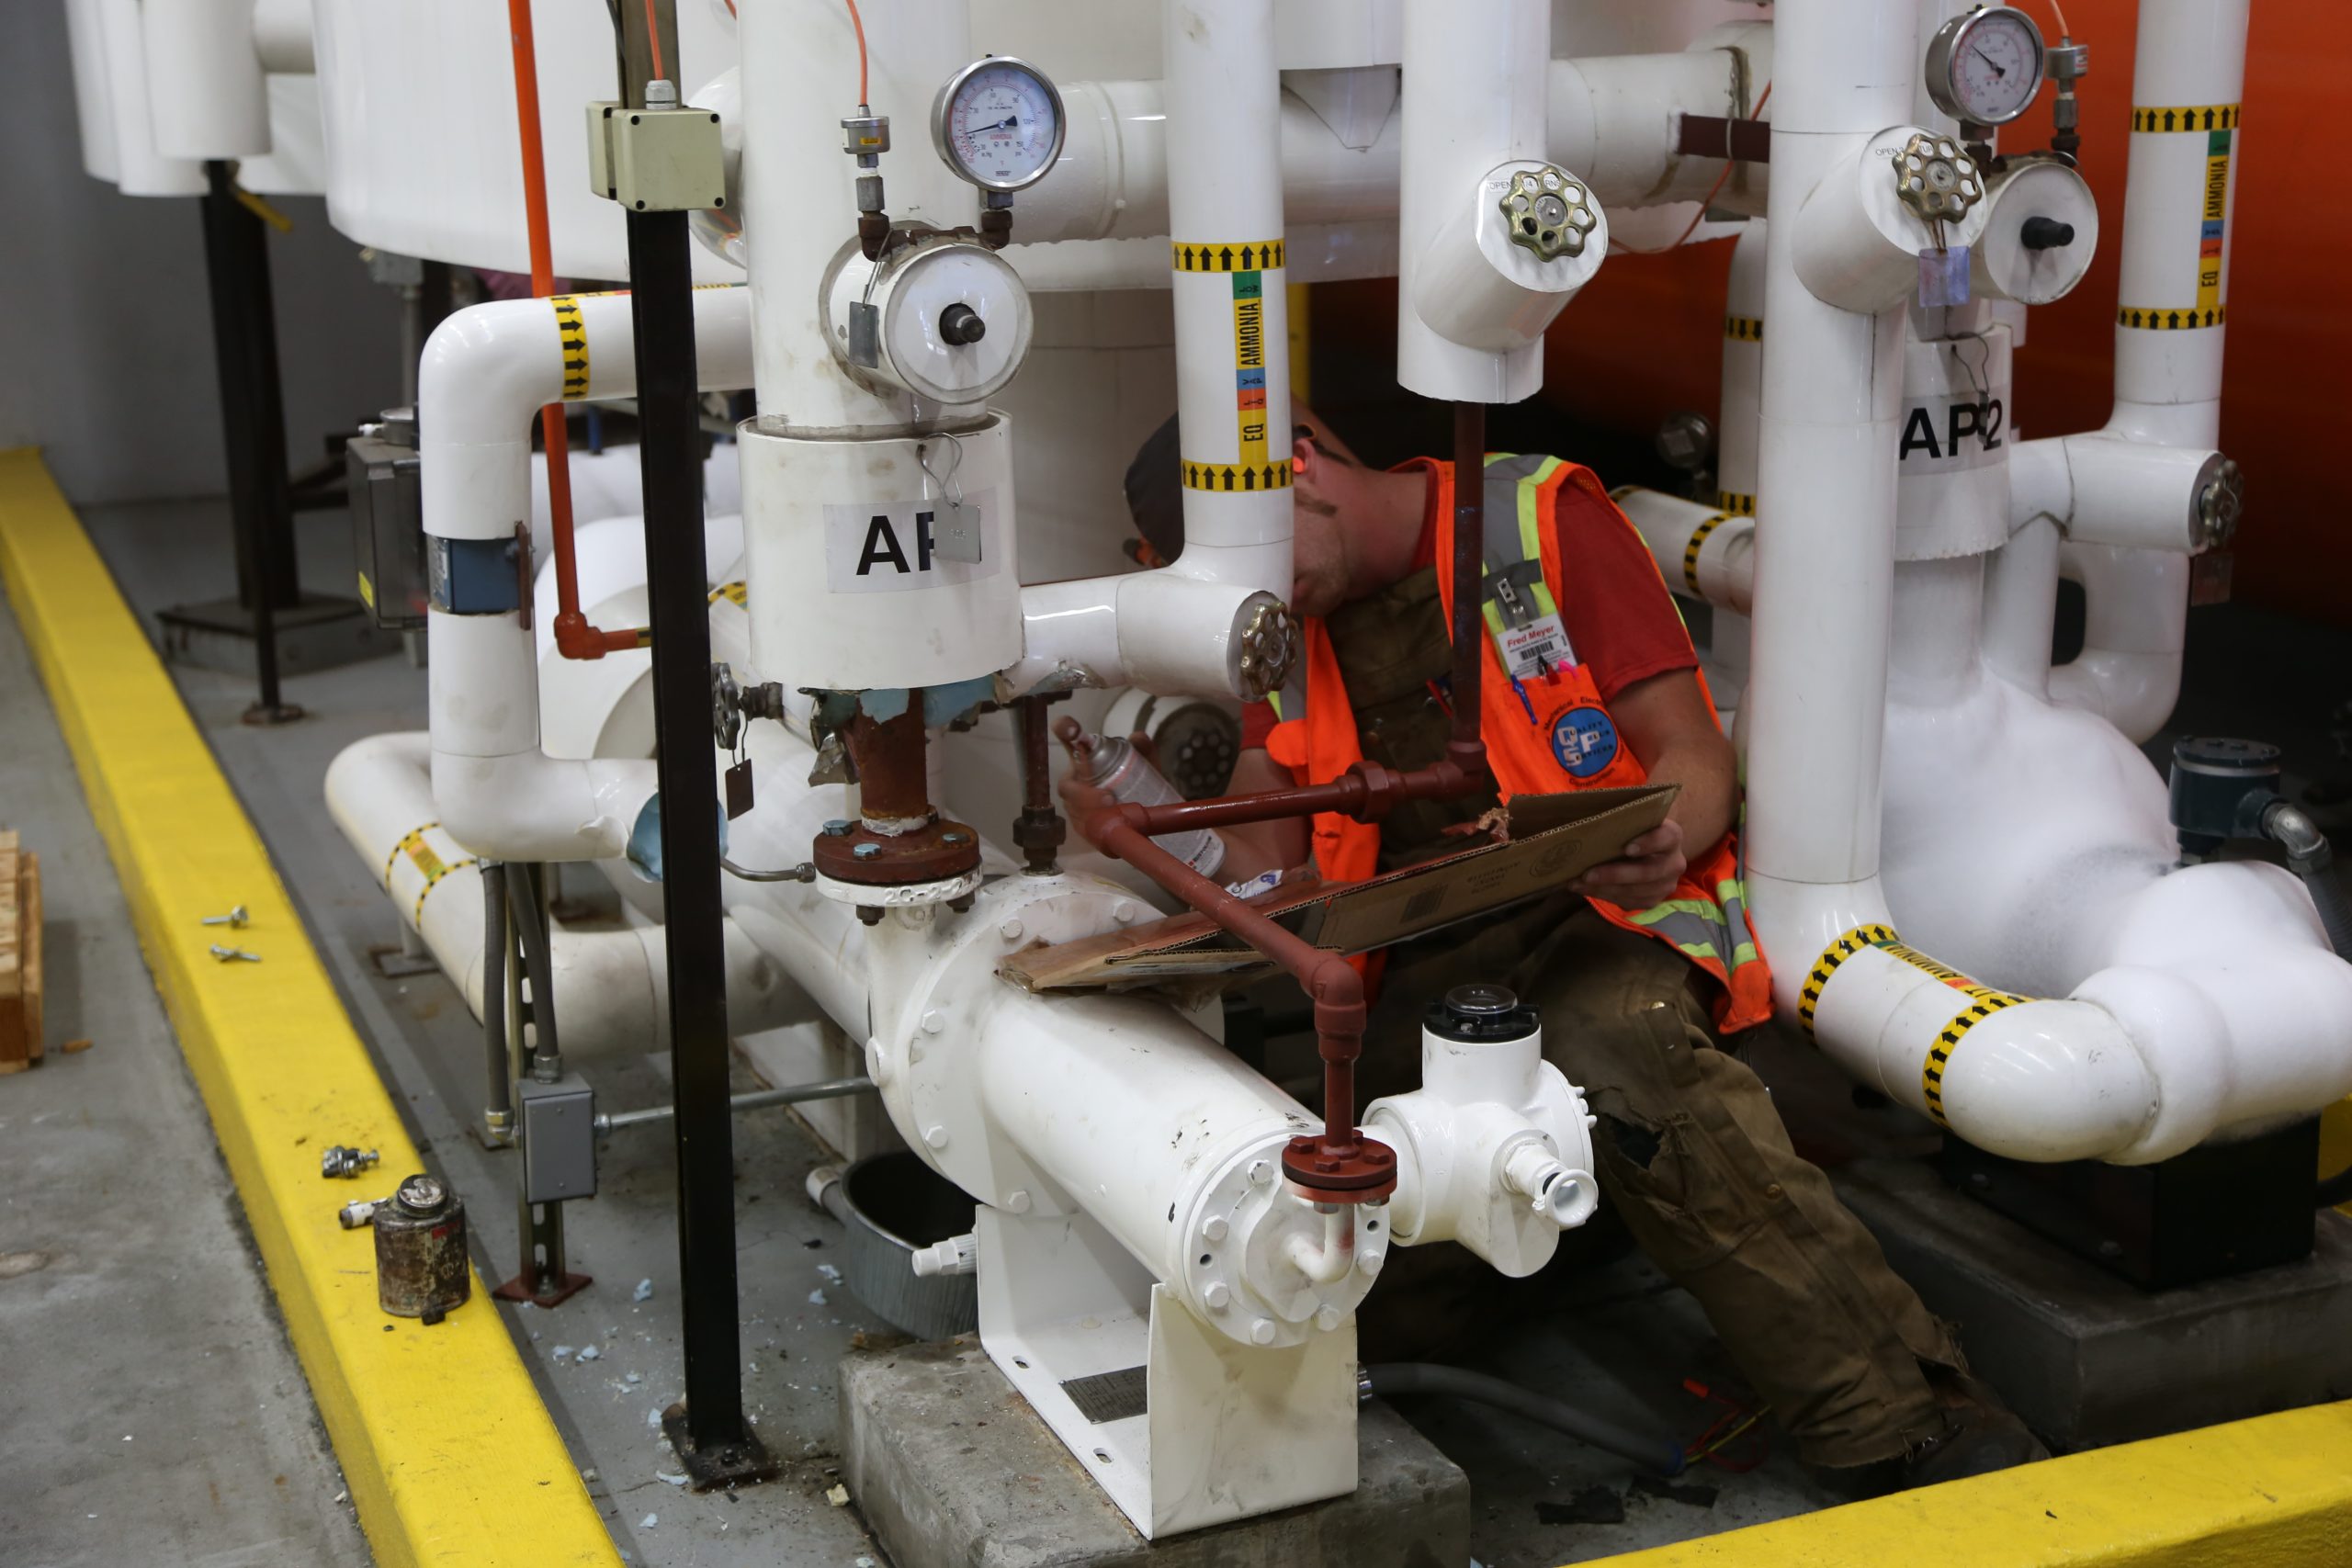
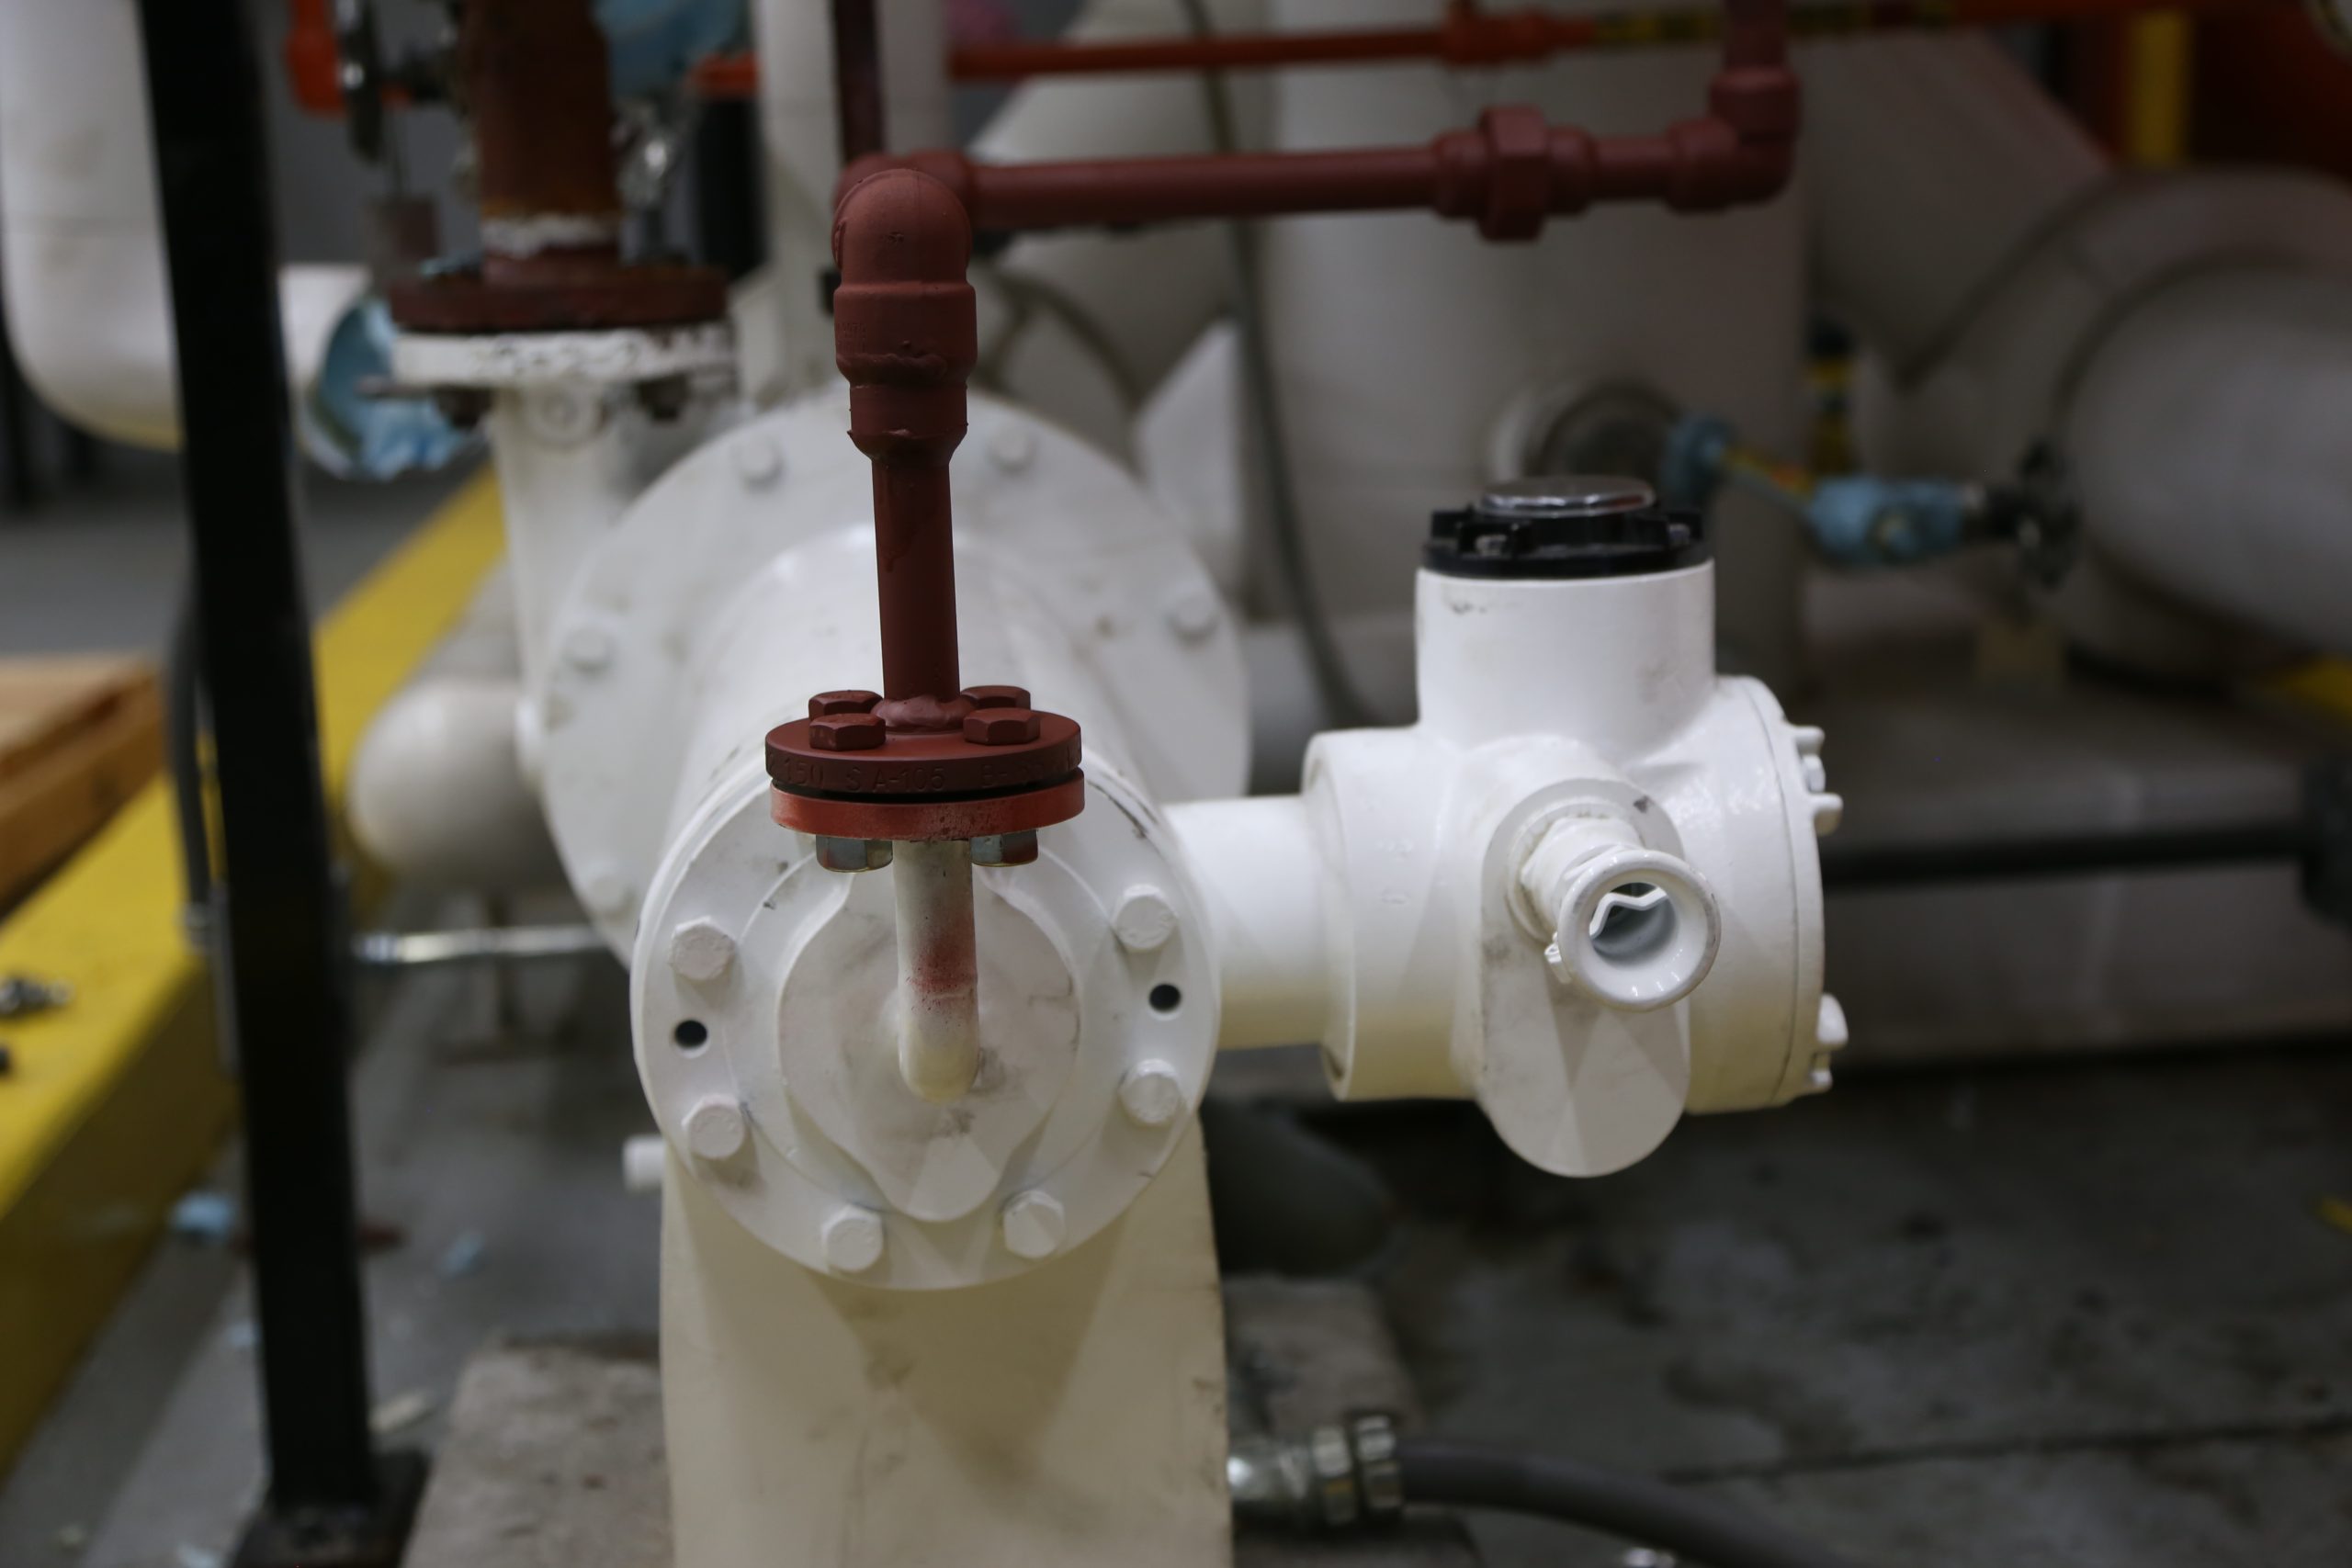
Cornell’s industrial refrigeration pumps are purpose-built for liquid overfeed and transfer. With more than 35 years in the industry, we back every Cornell pump with an industry-leading three-year warranty. Look for the angular, muscular frame to know it’s a Cornell pump.
50+
Years of
CB-series use
89%
Peak Pump
Efficiency
3 Year
Warranty on every
refrigeration pump
250 PSIG
Working pressure for both
HT and CB series
Refrigerants
Anhydrous and aqueous ammonia, halocarbons
CB series
Refrigerant emission-free sealing
HT series
Hermetic, drop-in
for CB
for CB
Improved NPSH
Low operating
speeds
speeds
Pump lines for Refrigeration
The right pump for every refrigeration application
Refrigeration Pumps
CB & HT Series
Available in two configurations: the emission-free CB-series and the hermetic HT-series for stable systems. Both deliver low operating speeds, enhanced NPSH performance, and an industry-leading warranty.
Emission-Free Seal, Hermetic, Drop-In Swap
Self-Priming Pumps
STX, STH & STL Series
Highly efficient and industry-renowned for durability, power, and energy efficiency. The patented Cycloseal® back plate technology makes them exceptionally durable. Easy to maintain and perfect for wastewater, slurry, and water transfer.
Cycloseal®, Slurry, Wastewater, Easy-Maintenance
CB series applications